
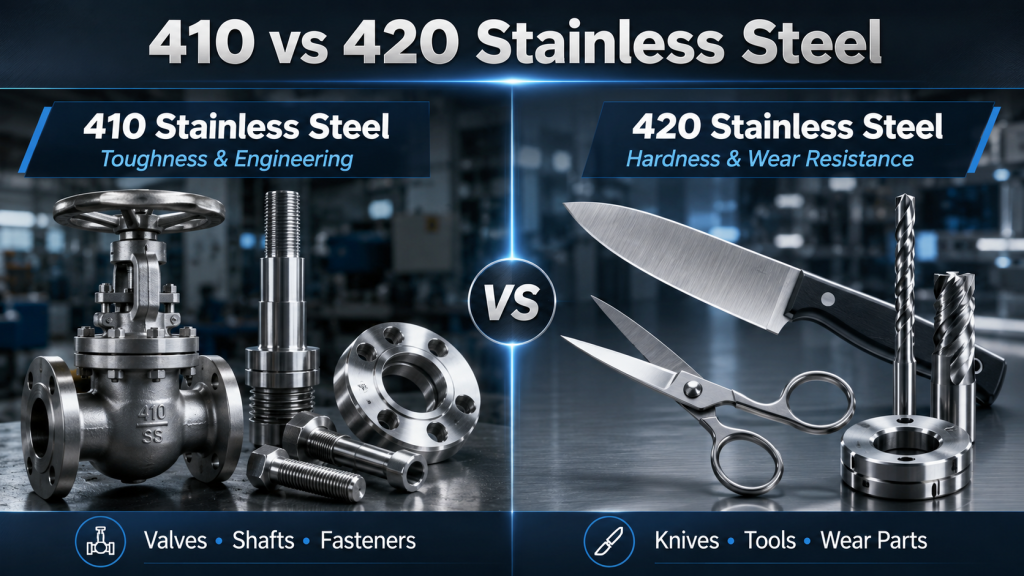
 The principal difference between 410 and 420 stainless steel is the carbon level and the hardness each alloy can develop after heat treatment. Grade 410 is a general-purpose martensitic stainless steel that normally provides a practical balance of toughness, strength, machinability and moderate corrosion resistance. Type 420 is a higher-carbon martensitic family designed to achieve greater hardness, wear resistance, polishability and edge retention.
This guide compares 410 vs 420 stainless steel by chemical composition, grade variants, heat treatment, hardness, toughness, wear resistance, corrosion behavior, welding, machining, surface finish, applications and international purchasing requirements.
Quick Answer: Should You Choose 410 or 420 Stainless Steel?
- Choose 410 stainless steel
when toughness, general mechanical strength, moderate hardness and easier machining are more important than maximum edge retention. - Choose 420 stainless steel
when the component needs higher hardness, wear resistance, polishability or cutting performance after heat treatment. - Choose 420J1 or EN 1.4021
for components requiring a lower-to-medium hardness range with a practical balance of formability and toughness. - Choose 420J2, EN 1.4028 or another higher-carbon variant
when greater hardness and wear resistance are required. - Do not substitute 410S for standard 410
when hardening is required. 410S is a low-carbon modification designed to minimize hardening.
410 vs 420 Stainless Steel at a Glance
| Comparison Factor | 410 Stainless Steel | 420 Stainless Steel |
|---|---|---|
| Stainless steel family | Martensitic stainless steel | Martensitic stainless steel |
| Common UNS designation | S41000 | S42000 |
| Main design priority | Toughness, mechanical strength and moderate hardness | Higher hardness, wear resistance and edge retention |
| Carbon requirement | Normally approximately 0.15% maximum under common flat-product requirements | ASTM Type 420 requires a higher carbon level; regional and commercial variants use different controlled ranges |
| Chromium range | Approximately 11.5–13.5% | Approximately 12–14% |
| Heat treatable | Yes | Yes |
| Potential final hardness | Moderate to high, depending on treatment | Normally higher, especially in higher-carbon 420 variants |
| Toughness | Generally better when compared at practical service conditions | Normally decreases as carbon and final hardness increase |
| Wear resistance | Moderate to good | Normally better after suitable hardening |
| Machinability | Generally easier in the annealed condition | More demanding as carbon and hardness increase |
| Formability | Better than higher-carbon 420 variants | Grade dependent; 420J1 is more formable than 420J2 |
| Weldability | Limited and procedure dependent | More difficult as carbon content increases |
| Magnetic response | Magnetic | Magnetic |
| Typical applications | Valves, shafts, axles, flanges, fasteners and pump components | Knives, scissors, instruments, press plates and wear-resistant parts |
Hardness values shown in mill or supplier literature are normally typical achievable results rather than universal guarantees. Final properties depend on carbon content, austenitizing, quenching, tempering, section thickness and the selected test method.
What Are 410 and 420 Stainless Steel?
410 Stainless Steel
Type 410, commonly identified as UNS S41000, is a general-purpose martensitic chromium stainless steel. It can be hardened and tempered to develop useful strength and hardness while retaining more toughness than many higher-carbon martensitic grades.
Typical uses include:
- Valve components
- Pump shafts
- Axles
- Flanges
- Fasteners
- Turbine and steam-system parts
- Mechanical hardware
- Press and brake components
420 Stainless Steel
Type 420, commonly identified as UNS S42000, describes a martensitic stainless steel family with more carbon than 410. Different 420 variants are produced for different combinations of hardness, toughness, wear resistance and polishability.
Typical uses include:
- Kitchen and professional knives
- Scissors
- Surgical instruments
- Cutting utensils
- Measuring tools
- Press plates
- Brake discs
- Wear-resistant mechanical parts
410S, 420J1 and 420J2 Are Not Interchangeable
410S Stainless Steel
410S stainless steel
is a low-carbon modification of 410 designed to remain softer, more ductile and less hardenable during cooling or welding.
410S can be useful for thermal-processing equipment, petrochemical components, press plates and fabricated parts requiring moderate oxidation resistance. It is not the correct substitute when the design requires the hardenability of standard 410.
420J1 Stainless Steel
420J1 stainless steel
is commonly associated with a lower-carbon 420 range. It offers a practical balance of hardenability, toughness, forming performance and polishability.
It may be considered for tableware, lower-to-medium hardness tools, mechanical components and selected medical or food-equipment parts after application review.
420J2 Stainless Steel
420J2 stainless steel
contains more carbon than 420J1 and can develop greater hardness, wear resistance and edge retention after appropriate heat treatment.
It is commonly evaluated for blades, scissors, cutting tools and wear-resistant components. The higher potential hardness normally reduces toughness and makes welding and forming more demanding.
Standards and Grade Cross-References
| Material | ASTM / UNS | Common EN Reference | Common JIS Reference | Purchasing Note |
|---|---|---|---|---|
| 410 | Type 410 / UNS S41000 | 1.4006 / X12Cr13 | SUS410 | Verify carbon limits, product form and delivery condition |
| 410S | Type 410S / UNS S41008 | 1.4000 is commonly used as a related low-carbon reference | SUS410S | Substantially different hardening behavior from standard 410 |
| Lower-carbon 420 | Type 420 / UNS S42000 family | 1.4021 / X20Cr13 | SUS420J1 | Common lower-to-medium hardness range |
| Medium-carbon 420 | Type 420 family | 1.4028 / X30Cr13 | SUS420J2 | Greater hardness and wear resistance |
| High-carbon martensitic grade | Confirm the manufacturer specification | 1.4034 / X46Cr13 | Confirm the applicable JIS designation | Commonly evaluated for high-hardness cutting tools |
ASTM, EN and JIS designations may have different chemistry, mechanical-property and delivery-condition requirements. Use one governing product standard in the purchase order.
Chemical Composition: Carbon Creates the Main Difference
| Élément | 410 Stainless Steel | 420 Stainless Steel Family | Practical Effect |
|---|---|---|---|
| Carbon | Normally up to approximately 0.15% | Higher than 410; exact controlled range depends on the selected 420 variant | Higher carbon increases hardenability, hardness and wear resistance but may reduce toughness and weldability |
| Chromium | Approximately 11.5–13.5% | Approximately 12–14% | Supports passivation and moderate corrosion resistance |
| Nickel | Low or limited | Low or limited | Neither is a conventional nickel-rich austenitic stainless steel |
| Molybdenum | Not normally required | Not normally required in standard 420 | Special martensitic grades may add molybdenum for additional corrosion or wear performance |
More carbon does not guarantee better overall performance. It increases the ability to form hard martensite, but the finished component must still balance hardness, toughness, corrosion resistance, dimensional stability and manufacturing cost.
Heat Treatment Determines the Final Properties
Both 410 and 420 are commonly supplied in a softer condition for cutting, forming or machining and then hardened and tempered when greater mechanical performance is required.
General Heat-Treatment Sequence
- Annealing or softening:
prepares the material for machining, forming or further processing. - Austenitizing:
heats the material into the grade-specific hardening range. - Quenching:
transforms the microstructure and develops martensitic hardness. - Tempering:
reduces excessive brittleness, relieves stress and adjusts the final balance of hardness and toughness.
Exact temperatures, holding times, quench media and tempering conditions should follow the applicable mill datasheet, component geometry, furnace capability and required final properties.
The specification should identify the exact 420 variant, required hardness range, test scale, test location, dimensional tolerance and whether straightening, grinding or polishing will occur after heat treatment.
Hardness, Edge Retention and Wear Resistance
After appropriate hardening and tempering, 420 normally develops greater hardness than 410 because of its higher carbon content.
The actual hardness obtained from either material depends on:
- Exact carbon content
- Austenitizing temperature
- Holding time
- Quench rate and quench medium
- Tempering temperature
- Section thickness
- Decarburization
- Hardness-test method and test location
Edge Retention
A suitable 420 variant is normally the better starting point when the component must maintain a sharpened edge. Higher hardness reduces plastic deformation and abrasive wear at the cutting edge.
Edge performance also depends on blade geometry, heat-treatment consistency, carbide distribution, grinding, sharpening angle and the type of material being cut.
Wear Resistance
420 normally provides better abrasive and adhesive wear resistance after suitable hardening. However, a component hardened excessively for its application may chip or crack under impact, misalignment or bending.
Toughness, Strength and Impact Loading
410 generally provides a more forgiving property balance where shock loading, torque, bending or impact resistance is important.
Common examples include:
- Pump shafts
- Valve stems
- Axles
- Fasteners
- Flanges
- Steam-service components
- General mechanical hardware
The comparison is not absolute. An incorrectly heat-treated 410 component can become brittle, while a correctly tempered 420 component can retain useful toughness. Final performance should be verified in the specified heat-treatment condition.
Corrosion Resistance: Is 420 Always Better?
No. 420 should not be described as universally more corrosion resistant than 410.
Both grades contain enough chromium to provide moderate resistance in water, steam and mild atmospheric environments when correctly heat treated, cleaned and finished. Actual corrosion performance depends on:
- Chromium and carbon balance
- Heat-treatment condition
- Chromium-carbide formation
- Surface roughness
- Grinding and polishing quality
- Passivation and cleanliness
- Iron contamination
- Chloride concentration
- Crevices and deposits
The strongest corrosion performance is normally obtained after appropriate heat treatment, fine grinding or polishing, and thorough removal of surface contamination.
Neither 410 nor 420 should be treated as a substitute for 316L in aggressive chloride service. Marine immersion, salt spray, hot brine and aggressive cleaning systems may require 316L, duplex or another higher-alloy stainless steel.
Welding 410 and 420 Stainless Steel
Traditional martensitic stainless steels have limited weldability because rapid cooling can create a hard and brittle heat-affected zone.
Welding 410
410 can be welded using a qualified procedure, but the project may require preheating, controlled heat input, a suitable filler metal, slow cooling and post-weld tempering.
Welding 420
420 becomes more difficult to weld as carbon content increases. High-carbon variants used for cutting tools are generally unsuitable for routine welded fabrication.
A welding specification should identify:
- Exact base-metal grade
- Joint design
- Section thickness
- Filler-metal requirement
- Preheat range
- Interpass-temperature control
- Post-weld heat treatment
- Final hardness and inspection criteria
Machining, Forming and Grinding
Machining
Both grades are normally machined in a softer condition before final hardening. Annealed 410 is generally easier to machine than higher-carbon 420.
Rigid equipment, sharp tooling, positive cutting action and suitable coolant help control heat generation, tool wear and poor surface quality.
Forming
410 generally provides better formability than high-carbon 420. Complex bending, drawing and stamping should be completed before hardening whenever practical.
420J1 normally forms more readily than 420J2 or high-carbon knife grades.
Grinding
Grinding after heat treatment controls dimensional accuracy, edge geometry and surface finish. Excessive grinding heat can cause tempering, surface burns, cracking and dimensional distortion.
Surface Finish and Polishability
Both 410 and 420 can be ground and polished, but 420 is widely selected for fine-polished and mirror-finish cutting tools and instruments.
Common requested surface conditions include:
- No.1 hot-rolled condition
- 2B cold-rolled finish
- BA or bright condition
- Ground finish
- Fine polished finish
- Mirror polish
- Hardened and tempered precision strip
A finish name alone may not be sufficient for critical visible, cutting or hygienic components. Buyers should approve a physical sample or specify roughness, polish direction, gloss and defect limits.
410 vs 420 Application Selection
| Application | Recommended Starting Grade | Main Selection Reason |
|---|---|---|
| Valve stem or valve component | 410 | Balance of strength, toughness and moderate corrosion resistance |
| Pump shaft | 410 or another application-specific martensitic grade | Mechanical loading, toughness and machinability |
| Axle or mechanical shaft | 410 | Better general toughness than higher-carbon 420 |
| Fastener | 410 after specification review | Mechanical strength and moderate corrosion resistance |
| Table knife or butter knife | 420J1 or another suitable lower-carbon 420 variant | Balanced formability, polishability and hardness |
| Kitchen knife blade | 420J2, EN 1.4034 or another knife-grade martensitic alloy | Higher hardness and edge retention |
| Scissors | 420J2 or another selected 420 variant | Cutting-edge performance and wear resistance |
| Surgical cutting instrument | Application-specific 420-type or higher-alloy martensitic grade | Hardness, polishability and validated corrosion performance |
| Press plate | 410, 420J1 or another specified variant | Required hardness, flatness and surface condition |
| Impact-loaded wear component | 410 or carefully tempered 420 | Toughness must be balanced against wear resistance |
Food-contact, medical and surgical suitability applies to the finished component and manufacturing process—not merely to the alloy name. Heat treatment, surface finishing, cleaning, validation and regulatory requirements must also be considered.
Product Forms and JUDE Supply Options
JUDE can review project requirements for 410-family and 420-family stainless steel materials, subject to grade, standard, dimensions, delivery condition and availability.
Stainless steel sheet and plate
for press plates, mechanical parts, tooling blanks and fabricated components.
Stainless steel coil
for continuous processing, blanking and high-volume manufacturing.
Stainless steel strip
for blades, clips, precision parts and narrow components.
Stainless steel strip processing
for slitting, leveling, rewinding and customized strip width.
Inspection and Quality Control
Martensitic stainless steel requires more than chemistry verification because final component performance depends strongly on heat treatment and hardness.
A project inspection plan may include:
- Grade and product-standard verification
- Mill test certificate review
- Heat-number traceability
- PMI or chemical analysis
- Carbon verification when grade separation is critical
- Hardness testing
- Microstructure examination
- Dimensional inspection
- Flatness and straightness inspection
- Surface-finish inspection
- Decarburization review
- Crack or nondestructive examination when required
- Packaging and material-marking review
Handheld XRF instruments may identify chromium and other alloying elements but can have limitations when separating grades whose main difference is carbon. Carbon-sensitive verification may require optical emission spectroscopy or another appropriate laboratory method.
Review selected JUDE
stainless steel inspection reports
when defining material documentation and traceability requirements.
How to Choose Between 410 and 420
1. Identify the Primary Failure Risk
Determine whether the component is more likely to fail from impact, bending and fatigue or from abrasive wear, edge deformation and surface damage.
2. Define the Required Hardness
State the target range, hardness scale, test method and test location. Do not use only the words “hard” or “fully hardened.”
3. Define the Required Toughness
Review shock loading, vibration, torque, misalignment and the consequences of chipping or cracking.
4. Describe the Corrosive Environment
Provide information about water, steam, humidity, food acids, cleaning chemicals, chlorides and operating temperature.
5. Confirm the Manufacturing Route
State whether the material will be cut, stamped, formed, machined, welded, heat treated, ground, polished or sharpened.
6. Select the Exact Grade Variant
Confirm 410, 410S, 420J1, 420J2, EN 1.4021, 1.4028, 1.4034 or another specified martensitic grade.
7. Define Final Inspection
Specify material traceability, chemical verification, hardness, flatness, surface finish, edge condition and nondestructive testing where required.
410 or 420 Stainless Steel RFQ Checklist
- Exact material:
410, 410S, 420, 420J1, 420J2, EN 1.4021, 1.4028, 1.4034 or another specified grade. - UNS, EN or JIS designation:
State the required designation rather than relying only on the family name. - Product standard:
ASTM A240/A240M, EN 10088-2, JIS G 4304, JIS G 4305 or another applicable standard. - Product form:
Sheet, plate, coil, strip, bar, blank or fabricated component. - Delivery condition:
Annealed, softened, hardened and tempered, or another specified condition. - Required hardness:
State the range, scale, test method and test location. - Dimensions:
Thickness, width, length, diameter and tolerances. - Flatness and straightness:
Define special limits for blades, press plates and precision strip. - Surface finish:
No.1, 2B, BA, ground, polished, mirror or an approved physical sample. - Edge condition:
Mill edge, slit edge, deburred, rounded, sharpened or precision ground. - Heat treatment:
Provide the required procedure or final property target. - Fabrication:
Cutting, blanking, slitting, bending, machining, welding, grinding or sharpening. - Service environment:
Moisture, steam, food acids, chemicals, chlorides and operating temperature. - Inspection:
MTC, PMI, carbon analysis, hardness report, dimensional report or third-party inspection. - Quantity and delivery:
Pieces, total weight, coil size, packaging, destination and required delivery date.
Common Purchasing Mistakes
420J1, 420J2, EN 1.4021, 1.4028 and 1.4034 can provide substantially different hardness, toughness and manufacturing behavior.
Sheet, coil and strip may be delivered annealed or in another processing condition. Final heat treatment may remain the component manufacturer’s responsibility.
A harder blade or wear part may chip, crack or fail under impact.
Both materials are normally magnetic. Magnet testing cannot reliably identify the exact grade.
The main difference may be carbon, which many handheld XRF instruments do not measure accurately.
Final suitability depends on the finished component, heat treatment, surface, cleaning process and applicable regulations.
Frequently Asked Questions
Is 420 stainless steel harder than 410?
Normally yes after suitable heat treatment. The higher carbon content of 420 allows it to develop greater hardness and wear resistance than 410.
Is 410 stainless steel tougher than 420?
410 generally provides better toughness than a higher-carbon 420 grade hardened to a high hardness level. The exact result depends on heat treatment, section size and final hardness.
Which grade is better for knives?
A suitable 420 variant is normally preferred because of its potential hardness, polishability and edge retention. Higher-performance knives may use other specialized martensitic stainless steels.
Which grade is better for pump shafts and valves?
410 is often the better starting point because it provides a practical balance of strength, toughness, machinability and moderate corrosion resistance.
Does 420 always have better corrosion resistance than 410?
No. Their corrosion performance overlaps and depends on chemistry, heat treatment, carbide formation, surface finish and exposure. Neither grade should be treated as equivalent to 316L in aggressive chloride service.
What is the difference between 420J1 and 420J2?
420J2 generally contains more carbon and can achieve greater hardness and wear resistance. 420J1 normally provides better formability and toughness.
Can 410 and 420 stainless steel be welded?
They can be welded only with appropriate precautions. Preheating, controlled heat input, filler selection and post-weld heat treatment may be required. Higher-carbon 420 variants are more difficult to weld.
Are 410 and 420 stainless steel magnetic?
Yes. Both are martensitic stainless steels and are normally magnetic in annealed and hardened conditions.
Can handheld XRF distinguish 410 from 420?
It may confirm similar chromium chemistry, but separating variants based mainly on carbon may require optical emission spectroscopy or another carbon-sensitive analytical method.
Conclusion
The decision between 410 vs 420 stainless steel is primarily a choice between toughness and hardness.
410 is normally better suited to valves, shafts, axles, fasteners and mechanical parts requiring moderate hardness, useful toughness and practical machinability.
420 is normally selected for knives, scissors, cutting utensils, instruments, press plates and wear components requiring greater hardness, polishability and edge retention.
The final result depends on more than the AISI number. Buyers should specify the exact variant, governing standard, carbon range, delivery condition, hardness, heat treatment, dimensions, finish and inspection requirements.
Request a 410 or 420 Stainless Steel Quotation
Send JUDE the exact grade, standard, product form, dimensions, delivery condition, required hardness, heat treatment, surface finish, fabrication requirements, inspection documents, quantity and destination.
For blade, tool or precision-strip projects, also provide the required edge condition, flatness, hardness test method and final application.
