
304L and 316L for Food and Detergent Tanks in Russia: A Fabricator’s Material Guide
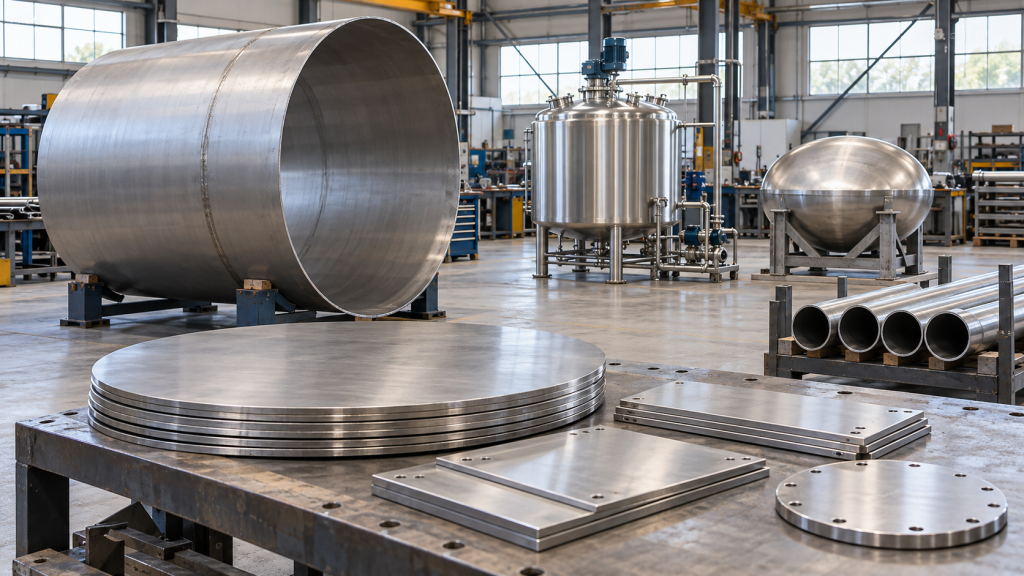 A food or detergent mixing tank starts as several different
material purchases: sheet for the shell, plate or circular
blanks for the heads, cut parts for the internals, and tube
or pipe for the liquid connections. Ordering all of them
simply as “food-grade stainless steel” leaves important
fabrication and inspection questions unanswered.
For equipment builders supplying plants in Russia,
304L and 316L stainless steel are candidate
materials for these welded components. The choice depends
on the product formulation, cleaning cycle and approved
equipment design. A material schedule should identify each
component before the supplier prices the order.
Procurement starting point:
evaluate 304L for compatible, relatively mild service and
316L where its molybdenum addition provides useful
additional corrosion resistance. Neither grade is a
universal choice for bleach, concentrated cleaning
chemicals or chloride-rich mixtures. This guide covers
raw-material purchasing; final material selection and
component thickness belong to the equipment design.
Which products create demand for 304L and 316L?
The following equipment types can generate sheet, plate,
blank and tubular-material enquiries. The examples describe
possible applications, rather than mandatory grades for
every machine.
| Product manufactured | Stainless steel components | Selection check before ordering |
|---|---|---|
| Food ingredient holding and blending tanks | Rolled shells, bottom or head blanks, lids, baffles and outlet connections | Assess the food formulation, residence time and cleaning cycle. Compatible mild service may support 304L. |
| Heated syrup, sauce and food premix vessels | Shell plate, formed-head blanks, mixing internals and jacket components | Evaluate product-side and jacket-side conditions separately, including temperature, pressure or vacuum and cleaning exposure. |
| Liquid detergent blending vessels | Wetted shells, baffles, addition ports, covers and transfer sections | Check concentrated ingredients and dosing stages as well as the diluted finished detergent. |
| Shampoo and liquid soap premix tanks | Tank shells, bottoms, lids and product-contact internals | Assess salts, pH, temperature and cleaning chemicals. The product name alone does not establish whether 304L or 316L is suitable. |
| Intermediate vessels and filling-machine feed tanks | Small shells, cones, covers, outlet stubs and connecting tube | Confirm the downstream equipment’s connection sizes, drainability and required contact-surface condition. |
| Replacement tank internals and maintenance parts | Replacement baffles, covers, approved shell inserts and short wetted pipe or tube sections | Identify the original material and reason for replacement. Pressure-boundary repairs require an approved repair specification. |
For background on welded food applications, see JUDE’s
304L food and dairy equipment guide
.
The purchasing focus here is how to divide a tank assembly
into clearly specified material lines.
Build the purchase list around five component groups
1. Shell sheet and plate: start with the developed cutting size
A fabricator rolls flat material into a cylindrical shell
and joins the edges. Quote the required flat dimensions,
thickness, quantity, dimensional tolerances and delivery
condition. Identify which face will contact the product
and whether it needs protective film or a specified finish.
Ask the workshop to approve the developed blank size,
trimming allowance and weld preparation. Buying a wider
plate may reduce the number of seams, but that benefit
must be checked against rolling capacity, handling limits
and material yield. An available stock thickness is not
a design calculation.
JUDE’s
stainless steel sheet and plate options
provide a starting point for an enquiry. Confirm the actual
grade, dimensions, finish and availability for the order.
2. Head blanks: distinguish starting plate from the finished head
A circular blank for a dished head is a fabrication input.
Its diameter is not simply the finished vessel diameter.
The head former should approve the starting thickness,
blank diameter, forming allowance and any orientation
requirements.
The purchase order should separate
starting material thickness from the
required minimum thickness after forming.
It should also state who is responsible for forming,
trimming, any required heat treatment and final inspection.
A quotation for a flat blank does not include those
operations unless they are expressly agreed.
3. Internals: separate flat cut parts from machined parts
Baffles, support plates and some impeller components can
be cut from flat stock. Shafts and machined hubs may require
bar or another product form under a different material
specification. Do not assign the plate specification to
every item in the assembly.
For cut parts, provide a dimensioned drawing or DXF file
with its revision, quantity, tolerances, edge condition and
marking requirements. Discuss suitable blank preparation
through JUDE’s
laser-cutting service
;
confirm process suitability for the particular material
and thickness.
4. Wetted connections: define tube or pipe explicitly
List outside diameter and wall thickness for tubing, or
the specified pipe size and wall designation for piping.
Add length, manufacturing route, end preparation and the
required internal surface. Fittings and connection geometry
need separate identification.
A polished appearance does not establish dimensional
compatibility or a hygienic specification. For an existing
Russian installation, use measured dimensions and the
approved connection drawing to avoid ordering a nominally
similar size that will not fit.
5. Maintenance pieces: preserve identification after cutting
Replacement plates, covers and inserts often reach a
workshop as small pieces. Agree how the heat number and
part number will remain traceable from the parent material
to each supplied item. Request a packing list that connects
those identifiers to the material certificate.
Where an original part has corroded, record the location
and operating conditions before specifying a replacement.
Repeating the original grade without reviewing the failure
may repeat the problem.
Choose 304L or 316L using the full process cycle
304L is identified by UNS S30403;
EN 1.4307 is a common corresponding designation.
316L is identified by UNS S31603;
EN 1.4404 is a common corresponding designation.
The low-carbon variants reduce susceptibility to
sensitization associated with welding. They still require
appropriate welding and surface restoration.
For identification references, see Outokumpu’s
Core 304L/4307
and
Supra 316L/4404
.
These references do not make different national product
specifications interchangeable.
316L contains molybdenum and generally offers better
resistance to localized corrosion than 304L in many
chloride-containing environments. Its suitability still
depends on the actual exposure. Before assigning either
grade to a detergent or food vessel, obtain:
- Product chemistry:
the complete formulation or relevant chemical composition,
concentrations, pH and chloride content where applicable. - Concentrated additions:
the composition and temperature near ingredient dosing
points before mixing is complete. - Cleaning conditions:
the cleaning agent, working concentration, temperature,
contact time and rinsing procedure. - Operating cycle:
normal and maximum temperatures, holding periods,
shutdown conditions and any stagnant zones.
Pay particular attention to hypochlorite bleach and strongly
acidic or chloride-rich formulations. Neither “detergent
service” nor “316L construction” establishes compatibility.
Use relevant corrosion data and, where necessary, testing
for the actual mixture; laboratory guidance such as
Outokumpu’s corrosion tables
must be interpreted within its stated conditions.
Specify the material standard for each product form
The purchase order needs a grade, a product specification
and its agreed edition. These are separate entries.
- Shells, flat head stock and plate internals:
ASTM A240/A240M
covers stainless steel plate, sheet and strip. Add the
selected grade, delivery condition, dimensional requirements
and any project-specific tests. - Sanitary tube:
ASTM A270/A270M
is a sanitary-tubing specification. State the required
dimensions and surface requirements rather than ordering
only “food-grade tube.” - Process pipe:
ASTM A312/A312M
addresses austenitic stainless steel pipe. Compliance alone
does not establish a finished hygienic contact surface.
The linked ASTM pages identify the scope of those
specifications; the contract must identify the edition
accepted for the project. Bar, fittings, finished heads
and completed vessels require their own applicable
requirements.
For a Russian drawing that specifies a GOST grade, GOST
product standard or TU technical specification, include
that exact designation in the enquiry. Ask the equipment
designer to approve any proposed ASTM or EN substitution.
A commercial equivalence table cannot establish compliance
with all chemistry, mechanical-property, testing and
documentation requirements.
Assign responsibility for finishing and inspection
A mill finish such as 2B or No.1 describes the supplied
surface. It does not by itself define the finished tank’s
cleanliness, weld condition or acceptable roughness.
If a roughness limit is required, specify the contact face,
Ra value and unit, measurement conditions, inspection
locations and the stage at which acceptance applies.
Separate the material supplier’s deliverables from the
fabricator’s work: raw-sheet condition, cut-edge condition,
weld finishing, removal of heat tint, cleaning and any
specified passivation. Agree who restores surfaces after
fabrication and how the result is accepted. ASTM’s
A380/A380M practice
addresses cleaning and related surface treatments, but
does not replace an equipment-specific acceptance plan.
For receiving inspection, check the ordered dimensions,
visible surface condition, heat identification and
certificate against the purchase order. Specify an
EN 10204 type 3.1 inspection certificate if that document
is required by the project, and confirm availability before
ordering. Raw-material documentation alone does not certify
the completed machine for food contact or pressure service.
Compare quotations using the same material schedule
A useful comparison separates the base material from
cutting, surface work, protection, inspection and packing.
Ask each supplier to quote the same drawing revision and
acceptance requirements.
- Dimensions and quantity:
confirm whether the quote covers full sheets, net-size
blanks or oversized blanks for later trimming. - Material utilization:
compare full-sheet nesting with cut-part supply;
establish whether useful remnants are included or retained. - Grade alternatives:
where the designer permits alternatives, request separate
304L and 316L lines for the same component and finish. - Traceability:
state any restriction on mixing heats and the
identification required on individually packed parts. - Delivery basis:
name the destination in Russia, requested delivery date,
packing needs and agreed delivery term and place.
For repeat tank production, a consistent blank schedule
can make quotations easier to compare and reduce workshop
sorting. Any claimed saving should be calculated from the
actual layout, fabrication work and accepted offer.
Send a component-based RFQ to JUDE Steel
Use the following template for a material enquiry.
Complete one line per component group and attach drawings
where available. Leave undecided requirements marked for
review rather than filling them with assumed values.
Subject: RFQ - 304L / 316L tank materials - Russia Equipment: [food mixing tank / detergent vessel / other] Project and drawing revision: [reference] Product and cleaning conditions: [attach process summary] For each material line: Component: [shell / head blank / internal / tube / repair piece] Grade and UNS or EN designation: [required grade] Product standard and edition: [project requirement] Product form and delivery condition: [sheet / plate / tube / other] Dimensions and tolerances: [mm; include drawing where needed] Quantity: [pieces, lengths or mass] Surface: [contact side, supplied finish, required acceptance] Processing: [cutting, edge preparation, protection and marking] Certificate and additional tests: [project requirement] For head blanks: [former-approved blank size and starting thickness] For tubing: [OD x wall, length, internal finish and end details] Delivery destination in Russia: [city and named place] Required delivery date and delivery term: [details] Please itemize material, processing, inspection and packing. Please identify any deviation from the requested specification.
Request a quote for your tank-material list.
Send JUDE Steel the grade, dimensions, quantity, surface
requirements and drawing revision. Ask for confirmation
of the available material, processing scope, certificates
and delivery basis for each line.
Material references:
JUDE 304L stainless steel
and
JUDE 316L stainless steel
.
Email:
support@jiscojude.com
.
Include your company name and a contact address for
the quotation.
Frequently asked questions
Can dual-certified 304/304L or 316/316L stock be accepted?
It may be accepted when the actual material certificate
demonstrates compliance with both claimed grades under
the required specification and the project permits it.
A supplier’s catalogue description or a handwritten
“dual grade” label is insufficient evidence.
Can handheld XRF confirm that a plate is an L grade?
No. Handheld XRF does not measure carbon, so it cannot
establish the low-carbon requirement that distinguishes
304L or 316L from the corresponding standard-carbon grade.
Use traceable certification and, where independent
confirmation is required, an agreed method capable of
measuring carbon.
Thermo Fisher explains the distinction between XRF,
LIBS and OES
.
Can certified offcuts be used for small replacement parts?
Potentially, if the project allows them and their identity,
certificate linkage, dimensions and condition remain
verifiable. An unidentified piece should not be accepted
merely because it looks like stainless steel or resembles
the original part.
Does the same roughness number make two surfaces interchangeable?
No. Ra is one measured characteristic. Surface defects,
finish direction, weld transitions and the measurement
procedure can also matter. The acceptance specification
should identify the required surface quality rather than
relying on a roughness number alone.
