
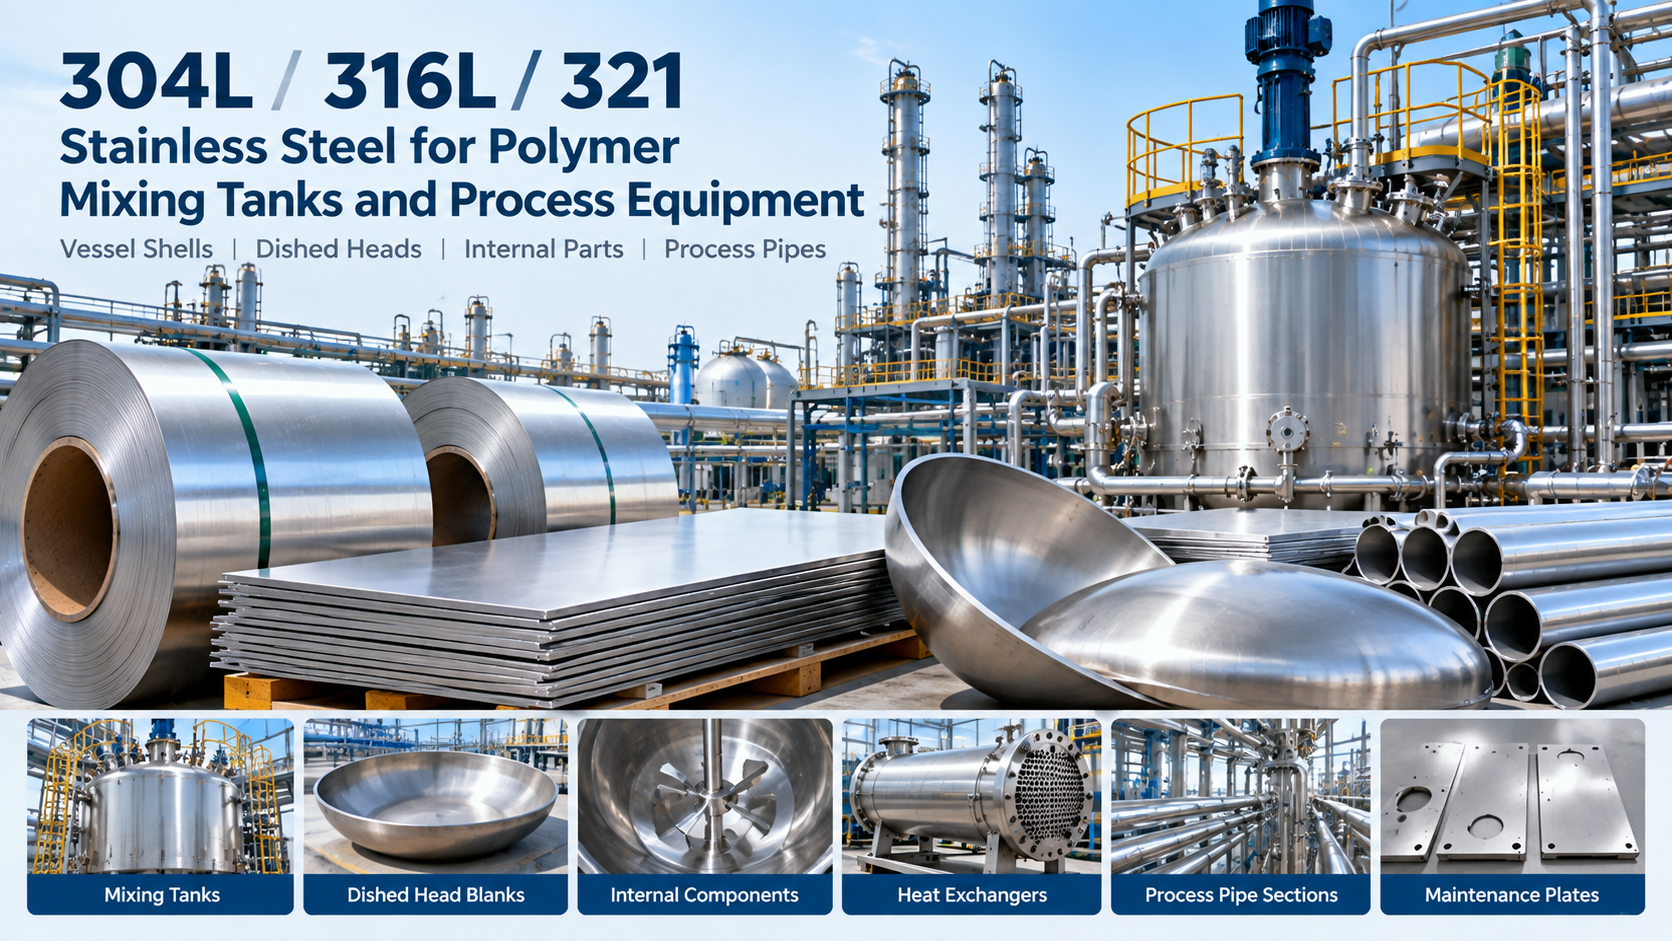
 Application Guide | Stainless Steel for Chemical Equipment Manufacturing
A fabricator building a jacketed polymer additive mixing tank does
not buy “chemical-grade stainless steel” as one unspecified item.
The material schedule may include shell plate, dished-head blanks,
internal baffles, nozzle reinforcement pads, removable covers
and process-contact connections. Each part has a different
fabrication route and may encounter a different environment.
For these projects, 304L, 316L and 321 are possible material
candidates, but their roles should not be confused. 304L is often
considered for compatible welded service. 316L may offer an
additional localized-corrosion margin in certain environments.
321 is a titanium-stabilized grade considered for selected
elevated-temperature duties rather than a universal upgrade
for chemical mixing equipment.
This guide is written for equipment OEMs, vessel fabricators,
engineering contractors and industrial buyers ordering stainless
steel flat products. Its primary focus is the raw material needed
to manufacture the equipment, not the sale of finished mixing
tanks or a guarantee of material suitability.
Quick Answer: Which Mixing Tank Parts Can Be Made from Stainless Steel Plate?
Subject to engineering approval, stainless steel sheet or plate
can be used to manufacture the following components:
- Rolled and welded vessel-shell sections
- Dished-head and bottom-head forming blanks
- Conical transition sections and fabricated outlet sections
- Internal baffles, supports and distribution plates
- Selected mixer mounting and reinforcement plates
- Nozzle reinforcement pads and fabricated attachments
- Maintenance covers and removable access panels
- Selected jacket-shell sections and utility-side panels
These parts may use different grades, thicknesses, finishes
and inspection requirements. A completed vessel or skid can
also require separately specified pipe, tube, forgings,
fasteners, gaskets, seals and rotating components.
For flat-material availability and cutting options, review
JUDE stainless steel sheet and plate.
Any requirement for formed finished heads, completed vessels
or other fabricated assemblies should be confirmed separately
before placing an order.
1. Start with the Finished Equipment, Not the Grade Name
Polymer-processing projects can include additive preparation
tanks, blending vessels, jacketed mixing tanks, intermediate
holding vessels and mixing modules incorporated into process
skids. Their operating conditions can differ considerably.
A vessel handling a compatible additive mixture at moderate
temperature should not automatically receive the same material
specification as equipment exposed to aggressive cleaning
chemicals or sustained elevated-temperature service.
The term “polymer” does not identify the full corrosive
environment.
Typical Stainless Steel Material Requirements
| Equipment or component | Raw material | Fabrication operation | Key purchasing check |
|---|---|---|---|
| Jacketed mixing tank shell | Stainless steel plate or sheet | Plate rolling and longitudinal welding | Grade, thickness, shell development and design code |
| Dished head or vessel bottom | Plate or cut forming blank | Pressing, spinning or other approved forming | Blank size, forming allowance and final thickness |
| Internal baffles and support plates | Sheet, plate or cut blanks | Profile cutting, forming and welding | Process exposure, mechanical loading and weld details |
| Nozzle reinforcement pad | Plate or profiled blank | Cutting, fit-up and welding | Approved reinforcement detail and material specification |
| Access cover or maintenance panel | Sheet or plate | Cutting, drilling and edge preparation | Pressure duty, gasket interface and surface condition |
| Selected jacket section | Sheet or plate | Rolling or formed-panel fabrication | Heating or cooling medium, pressure and temperature |
| Process-contact pipe spool | Finished stainless steel pipe | Pipe cutting, fitting and welding | Pipe standard, schedule, NPS, grade and test requirements |
The table is a material planning guide, not an equipment design.
Pressure-retaining components and structural details must be
approved by the responsible engineer under the governing
project specification.
2. 304L vs 316L vs 321: What Changes the Material Decision?
The first question is not which grade is “best.” It is which
corrosion, fabrication or temperature requirement controls
the component.
| Класс | Common designation | Selection consideration | Do not assume |
|---|---|---|---|
| 304L | UNS S30403; EN 1.4307; SUS304L | Welded components in compatible process and cleaning environments | Suitable for every chemical, chloride concentration or cleaning cycle |
| 316L | UNS S31603; EN 1.4404; SUS316L | Additional resistance to pitting and crevice corrosion in many relevant environments | Immune to chloride attack, stress-corrosion cracking or aggressive acids |
| 321 | UNS S32100; EN 1.4541; SUS321 | Titanium stabilization where elevated-temperature exposure and sensitization resistance justify it | Automatically superior to 316L or suitable for every high-temperature pressure application |
When 304L May Be Considered
Type 304L is a low-carbon chromium-nickel austenitic stainless
steel. Its lower carbon specification reduces susceptibility
to chromium-carbide precipitation during welding compared
with a corresponding higher-carbon condition.
In a compatible environment, it may be considered for
welded shell sections, internal plates, vessel covers
and other fabricated tank components.
The material review must include the actual process liquid,
minor constituents, cleaning agents, temperature, chloride
level and periods when solution can remain trapped.
See the JUDE reference for
304L stainless steel in chemical equipment.
When 316L May Be the More Appropriate Candidate
316L adds molybdenum to the low-carbon austenitic alloy system.
This often improves resistance to localized corrosion,
particularly pitting and crevice corrosion under relevant
chloride-containing conditions.
In a mixing tank, the review should pay attention to
concentrated chemical addition points, liquid-retaining
joints, deposits, crevices and cleaning operations.
The nominal composition of the fully mixed product may not
represent every local exposure during operation.
Where 304L does not provide the required corrosion margin,
316L may be assessed. However, 316L should not be assumed
suitable for all hot chloride solutions, concentrated acids
or other aggressive process environments. A higher-alloy
material may be necessary.
For the alloy-selection background, read
316L stainless steel for chemical and refinery equipment.
Where Type 321 Actually Fits
Type 321 is titanium-stabilized austenitic stainless steel.
Stabilization can reduce susceptibility to sensitization-related
intergranular corrosion after certain elevated-temperature
exposures.
It should not be specified for every jacketed mixing tank
merely because the vessel has a heating jacket.
Many jacketed vessels operate under conditions where 321’s
stabilization does not provide the controlling material benefit.
Where a process includes sustained or repeated
elevated-temperature exposure, engineers may evaluate
321 for selected welded components. The decision must also
address oxidation, process corrosion, strength, thermal
history and applicable code requirements.
If high-temperature creep or stress-rupture strength
controls the design, the engineer must evaluate an
appropriate material such as 321H or another specified
high-temperature alloy rather than treating standard
321 as an automatic substitute.
For additional guidance, see
JUDE’s technical article on 321 stainless steel.
3. Separate the Wetted Vessel from the Heating or Cooling Jacket
A jacketed mixing vessel can have at least two distinct
service environments:
- Process side: The product, additives,
intermediates, contaminants and cleaning fluids contacting
the inner vessel and its internals. - Jacket side: Water, thermal fluid, steam
or another approved heating or cooling medium, depending
on the equipment design.
The materials for these two circuits should be reviewed
separately. A grade selected for the process-contact
surface does not automatically become the correct material
for the jacket, and vice versa.
Where different stainless steel grades are proposed within
one assembly, the engineer should review the interface,
weld procedure, differential thermal expansion, corrosion
exposure and inspection requirements. A mixed-grade design
is an engineering decision, not a purchasing shortcut.
4. Vessel Shell Plate: Five Checks Before Rolling
The shell often begins as a flat plate cut to the required
developed dimensions and then rolled into a cylindrical
section. Purchasing errors at this stage can affect
fit-up, weld preparation and material traceability.
- Confirm the approved grade and product standard.
Record the required material designation and edition,
not simply “stainless steel 316L.” - Confirm the required thickness.
Account for the design calculation, corrosion allowance
if specified, permitted material tolerance and any
project-specific fabrication requirement. - Confirm developed dimensions.
Use the approved fabrication drawing rather than
estimating a flat blank from nominal vessel diameter alone. - Confirm surface and edge condition.
Identify the supplied plate finish, weld-edge preparation,
handling restrictions and protection requirements. - Preserve traceability.
Maintain identification between the parent plate,
cut shell blank, material certificate and completed
fabrication records as required by the quality plan.
For laser-cut plate and profile requirements, review
JUDE’s laser cutting service.
Available equipment capability, cutting tolerance,
maximum dimensions and edge quality must be confirmed
for the particular material and order.
5. Dished Head Blanks: The Purchase Size Is Not the Finished Head Size
A dished head is not purchased simply by quoting the
finished vessel diameter and plate grade. The head
manufacturer determines the appropriate blank dimensions
from the approved head geometry and forming procedure.
Depending on the design, the head may be manufactured
by pressing, spinning or another qualified process.
Forming can change local thickness, especially in
high-strain regions.
Before ordering plate or a circular blank, confirm:
- Head type and approved drawing number
- Starting plate thickness and minimum required
finished thickness - Calculated blank diameter and dimensional tolerance
- Grade, product specification and delivery condition
- Forming method, possible intermediate operations
and required heat-treatment evaluation - Any specified nondestructive examination,
surface inspection or supplementary testing - Heat-number identification after cutting and forming
A flat-material supplier can discuss plate and blank
requirements, but the approved head dimensions and
forming acceptance criteria must come from the
responsible fabricator and design documentation.
6. Internal Baffles, Reinforcement Pads and Maintenance Covers
Internal Baffles and Support Plates
Baffles can influence mixing performance and may experience
fluid forces, vibration, deposits and localized chemical
exposure. Their thickness, attachment design and material
selection require engineering review.
For raw-material purchasing, identify each baffle’s
drawing number, grade, plate thickness, profile,
quantity and edge condition. Where the baffle
contacts the process liquid, its corrosion suitability
must be assessed for that specific exposure.
Nozzle Reinforcement and Mounting Plates
Nozzle reinforcement pads are not simply generic cut
washers. Their geometry and permitted material are
part of the vessel’s approved design.
Specify the exact drawing revision, required material,
cutout profile and acceptance criteria. Avoid changing
the grade or thickness solely to simplify stock
consolidation without engineering approval.
Access Covers and Maintenance Panels
A removable panel may appear less demanding than the
vessel shell, but its requirements depend on whether
it retains pressure, contacts chemicals, forms a
gasketed boundary or must withstand repeated handling.
A non-pressure-retaining guard is not governed by
the same requirements as a pressure-retaining
manway cover. Keep these items separate in
the material schedule.
7. Specify the Correct Material Standard and Product Form
A complete order identifies both the alloy designation
and the material product specification. A grade name
alone is not a complete purchasing standard.
| Product form | Relevant reference | Procurement distinction |
|---|---|---|
| Stainless plate, sheet and strip | ASTM A240/A240M | Check grade, product condition and relevant requirements |
| General flat-product requirements | ASTM A480/A480M | Apply the required dimensional, identification and general requirements |
| EN flat products | EN 10088-2 | Specify the exact EN grade and delivery requirements |
| JIS hot-rolled flat products | JIS G 4304 | Use the required grade and relevant hot-rolled product specification |
| JIS cold-rolled flat products | JIS G 4305 | Use the required grade and relevant cold-rolled product specification |
| Applicable austenitic stainless process pipe | ASTM A312/A312M | Pipe is not certified by a flat-plate specification |
For pressure equipment governed by an ASME code,
the project may require an applicable ASME material
specification, such as SA-240, and compliance with
the code’s material and fabrication provisions.
An ASTM A240 certificate alone should not be assumed
to establish complete code compliance.
The exact standard edition, measurement system,
inspection requirements and any permitted substitutions
must be defined by the purchaser and project specification.
Official references:
ASTM A240/A240M,
ASTM A480/A480M and
ASTM A312/A312M.
8. Material Certificates, PMI and Mixed-Grade Fabrication
A vessel project may require a material test certificate,
heat-number traceability, chemical analysis, mechanical
test results and additional inspection documentation.
The exact requirements depend on the purchase
specification and applicable equipment code.
Positive material identification (PMI) can help detect
certain alloy mix-ups, but the selected method has
limitations. Conventional handheld XRF can identify
elements such as chromium, nickel and molybdenum;
it cannot directly establish the low carbon limit
that distinguishes 304L from 304 or 316L from 316.
Where low-carbon verification is required, the project
must specify a suitable analytical method and
acceptance procedure. PMI does not replace every
requirement of the mill certificate.
More background is available in
JUDE’s stainless steel testing guide.
If an assembly contains more than one grade,
the purchaser should define how identification,
segregation and traceability will be maintained
during cutting and fabrication.
9. Example Material Schedule for a Polymer Mixing Tank RFQ
The following is an illustrative bill-of-materials
structure. It contains no assumed thickness,
quantity or final grade approval. Replace every
blank with the project’s actual drawing and
procurement requirements.
| Item | Component | Material to quote | Information to supply |
|---|---|---|---|
| 01 | Vessel shell | Approved 304L / 316L / alternative plate | Grade, standard, thickness, developed width, length, quantity |
| 02 | Dished-head blank | Approved stainless plate or circular blank | Starting thickness, blank diameter, forming drawing, quantity |
| 03 | Internal baffles | Approved stainless cut blanks | Grade, profile drawing, thickness, finish, quantity |
| 04 | Nozzle reinforcement | Approved plate blanks | Grade, drawing revision, cutout geometry, quantity |
| 05 | Maintenance cover | Approved sheet or plate | Pressure duty, grade, profile, gasket interface, quantity |
| 06 | Selected hot-zone component | 321 / 321H / alternative only if specified | Temperature duty, product standard, engineering approval |
| 07 | Process pipe spool | Separately specified finished pipe | Pipe grade, standard, NPS, schedule, length and tests |
The schedule does not mean that each tank needs all
three stainless steel grades. A project may use only
one approved grade, or may require other alloys
or non-metallic materials.
10. What Equipment Buyers Should Send Before Requesting a Quote
For a useful export quotation, the material supplier
needs more than the equipment name.
Prepare a consolidated RFQ that identifies:
- Project and equipment: Mixing tank,
additive preparation vessel, blending module
or other component application. - Drawing package: Item numbers,
approved revisions, flat blank layouts
and required cut profiles. - Grade and standard: Exact UNS,
EN or JIS grade and applicable product
specification, including edition where required. - Dimensions: Thickness,
width, length, blank diameter, quantity and
applicable tolerances. - Material condition: Required
surface finish, edge condition, flatness and
any special fabrication conditions. - Documentation: Required
MTC or inspection certificate, heat traceability,
PMI or supplementary testing if applicable. - Logistics: Destination,
required delivery date, packaging preferences
and requested Incoterms. - Technical review: Any
approved alternatives or unresolved
material-selection questions.
For projects supplying Nizhnekamsk, Tatarstan
or other industrial destinations in Russia,
include the exact destination and any
project-required GOST, technical specification
or regulatory documentation. Any proposed
equivalence or substitution should be
approved by the responsible project party.
Do not assume that a Western material designation
automatically satisfies every Russian or
Eurasian project approval requirement.
Applicable documentation and trade feasibility
must be confirmed for the order.
Frequently Asked Questions
Can 304L and 316L be used in different parts of the same mixing tank?
Potentially, but this requires engineering approval.
The corrosion environment, mixed-metal welds,
filler selection, joint design and inspection
requirements must be reviewed. Upgrading one
part to 316L does not upgrade all remaining
304L wetted surfaces.
Does a heating jacket mean the vessel needs 321 stainless steel?
No. Jacket temperature, process temperature,
exposure duration, corrosion mechanism and
design requirements determine whether a
stabilized grade has a useful role.
The presence of a jacket alone is
not a material-selection criterion.
Can JUDE quote a circular plate blank for a dished head?
A circular blank inquiry can be submitted
for supply and processing review.
Provide the approved blank diameter,
starting thickness, grade, product standard
and quantity. Any cutting capability,
availability or special tolerance
must be confirmed in the quotation.
Can the supplier determine finished head thickness from the original plate thickness?
Not reliably from the starting thickness
alone. Final thickness depends on head
geometry, forming process and deformation.
The approved forming calculation and
finished-part inspection requirements
belong to the fabricator and equipment designer.
Is an ASTM A240 certificate enough for a pressure vessel?
Not by itself. The applicable pressure-equipment
code can impose additional material, design,
fabrication, examination and documentation
requirements. Verify the approved code material
specification and all project requirements
before purchasing the plate.
Can handheld XRF confirm that stainless steel is the L grade?
Conventional handheld XRF does not directly
measure carbon. It cannot by itself reliably
distinguish 304 from 304L or 316 from 316L
where the distinguishing requirement is
the carbon limit. Use an appropriate
certificate and specified verification method.
What if the customer drawing lists a GOST grade instead of ASTM or EN?
Retain the exact original designation and
standard in the inquiry. Ask the project
engineer to approve any proposed alternative.
Commercially similar grades are not
automatically interchangeable across
different product specifications.
Can one purchase order cover shell plate, head blanks and baffle blanks?
Yes, a consolidated material schedule
can group several line items.
However, each item should retain its
own grade, specification, dimensions,
quantity, inspection requirements
and traceability identity.
Request Stainless Steel Plate and Cut Blanks for Your Mixing Tank Project
JUDE works with industrial buyers sourcing
stainless steel flat products and related
processing requirements. For jacketed
mixing tank manufacturing, send a line-item
material schedule for the shell plate,
head-forming blanks, internal baffles,
reinforcement plates or covers you
need to purchase.
Please include the approved grade,
standard, dimensions, quantity,
inspection documents and destination.
If 321 is requested for a hot-zone
component, identify the temperature
duty and project material specification.
Request a quotation:
Contact JUDE Steel
Email your BOM or drawings:
support@jiscojude.com
Useful purchasing note:
JUDE’s quotation should confirm
the products, grades, dimensions,
processing scope, testing,
certification, commercial terms
and delivery feasibility for your
specific order. Finished equipment
manufacturing is not implied by
the supply of flat steel products.
Technical disclaimer: This guide provides
preliminary material-procurement information.
It is not a vessel design, corrosion approval,
welding procedure, code certification or
guarantee of suitability. The equipment
designer, fabricator and project specifications
govern final material selection and acceptance.
