
How to Test Stainless Steel: The Ultimate Guide
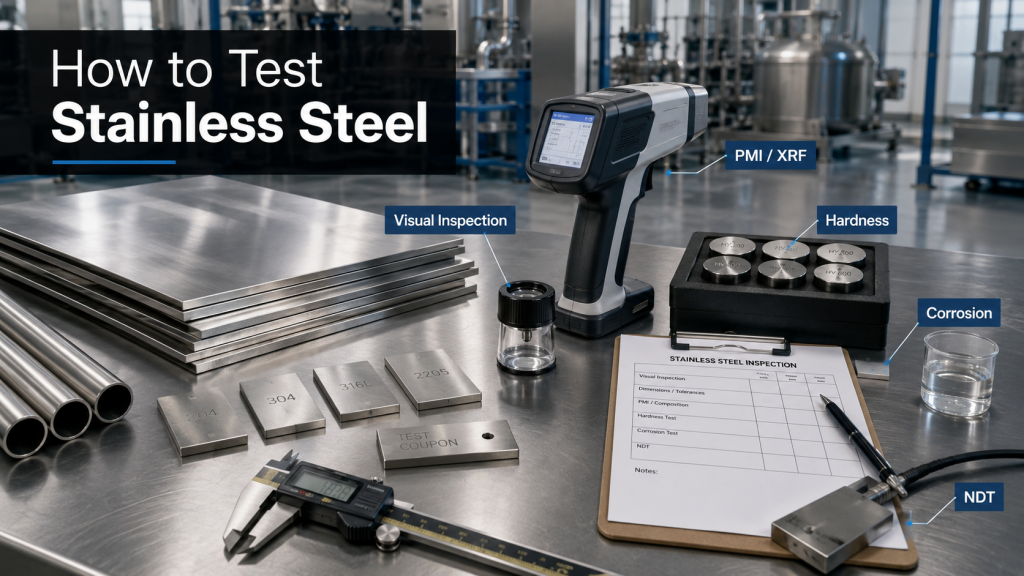
Stainless steel testing combines material identification, dimensional inspection, mechanical testing, corrosion evaluation and traceability verification.
Stainless steel cannot be identified reliably by appearance alone. Different grades may have almost identical surfaces while containing substantially different amounts of chromium, nickel, molybdenum, carbon, nitrogen and other alloying elements.
A polished sheet of 201 stainless steel may look similar to 304. Grade 304 and 316 can appear almost identical, although 316 normally contains molybdenum and offers stronger resistance in many chloride environments. Standard 304 and low-carbon 304L are also visually indistinguishable.
Selecting or accepting the wrong grade can cause premature corrosion, welding problems, incorrect mechanical properties, failed inspections, production delays and expensive equipment replacement.
This guide explains how to test stainless steel using simple field checks and professional laboratory methods. It covers visual inspection, dimensional testing, certificate verification, magnet tests, chemical spot tests, PMI, handheld XRF, OES, LIBS, combustion analysis, hardness testing, tensile testing, metallography, corrosion testing, surface inspection and nondestructive examination.
Quick Answer: What Is the Best Way to Test Stainless Steel?
For routine industrial purchasing, the most practical verification package is:
Material certificate and heat-number verification + dimensional and surface inspection + PMI/XRF testing.
Handheld XRF is highly useful for identifying alloying elements such as chromium, nickel, molybdenum and manganese. However, conventional handheld XRF cannot directly measure carbon. It therefore cannot reliably distinguish low-carbon grades such as 304L from 304 or 316L from 316.
When carbon content, nitrogen content, mechanical properties, corrosion resistance or safety-code compliance is critical, use a qualified laboratory and the test method specified by the applicable product standard.
Why Is Stainless Steel Testing Important?
Stainless steel is a family of corrosion-resistant alloys rather than one single material. Grade selection affects corrosion resistance, strength, weldability, formability, magnetic response, heat resistance and service life.
Testing may be required to:
- Confirm that the delivered grade matches the purchase order
- Prevent accidental material substitution or warehouse mixing
- Verify chromium, nickel, molybdenum and other alloy contents
- Confirm low-carbon or nitrogen-alloyed grades
- Check hardness, tensile strength and elongation
- Evaluate pitting, crevice or intergranular corrosion resistance
- Inspect welds for cracks, lack of fusion, porosity or other discontinuities
- Verify surface finish, roughness, cleanliness and passivation
- Maintain heat-number traceability
- Meet pressure-vessel, piping, food, pharmaceutical, marine or customer requirements
The required level of testing depends on the risk of failure. Decorative sheet normally requires less testing than pressure-retaining chemical equipment, medical components, offshore piping or safety-critical fasteners.
Stainless Steel Testing Methods at a Glance
| Testing Method | What It Checks | Typical Use | Main Limitation |
|---|---|---|---|
| Visual inspection | Surface defects, finish, labels, rust and damage | Initial incoming inspection | Cannot confirm grade or chemistry |
| Dimensional inspection | Thickness, width, length, flatness and edge condition | Sheet, plate, coil and strip acceptance | Does not identify alloy grade |
| Magnet test | Approximate magnetic response | Quick separation of some alloy families | Cannot reliably identify a specific grade |
| Spark test | Approximate alloy family and carbon behavior | Rough workshop screening | Subjective, destructive and unsuitable for final acceptance |
| Chemical spot test | Presence of selected elements such as molybdenum | Approximate 304/316 screening | Usually qualitative rather than fully quantitative |
| Handheld XRF | Cr, Ni, Mo, Mn and many alloying elements | Rapid field PMI and alloy sorting | Cannot directly measure carbon |
| Handheld LIBS | Alloy chemistry, including carbon on suitable instruments | Low-carbon grade separation and field PMI | Creates a small surface mark and requires proper calibration |
| Spark OES | Detailed chemical composition, including carbon | Professional grade verification | Requires surface preparation and creates a small burn spot |
| Combustion analysis | Carbon and sulfur | Confirming L grades and full laboratory chemistry | Requires representative sampling and laboratory equipment |
| Hardness test | Material condition and resistance to indentation | Annealed, cold-worked, martensitic and PH grades | Hardness alone does not confirm grade |
| Tensile test | Yield strength, tensile strength and elongation | Mechanical-property certification | Destructive and requires a prepared specimen |
| Metallography | Microstructure, grain size, phases and defects | Failure analysis and process qualification | Requires specimen preparation and expert interpretation |
| Corrosion test | Resistance under defined laboratory conditions | Alloy comparison and project qualification | Laboratory results do not automatically predict every service environment |
| Liquid penetrant testing | Surface-breaking discontinuities | Welds and nonporous components | Cannot detect deep internal defects |
| Ultrasonic testing | Thickness and internal discontinuities | Plate, pipe, forgings and welds | Requires suitable calibration and trained personnel |
1. Visual and Dimensional Inspection
Visual and dimensional inspection should be completed before advanced testing. It can identify obvious nonconformities and prevent unnecessary laboratory work.
What Should Be Checked Visually?
- Grade labels and product markings
- Heat number and batch identification
- Surface finish such as No.1, 2B, BA, No.4 or mirror
- Rust stains, discoloration and embedded iron contamination
- Scratches, dents, laminations, pits and handling damage
- Protective-film condition
- Coil telescoping, edge damage and packaging condition
- Weld heat tint and incomplete cleaning
Dimensional Inspection Tools
Depending on the product, inspectors may use:
- Calipers
- Outside micrometers
- Ultrasonic thickness gauges
- Steel rules and measuring tapes
- Flatness tables and straightedges
- Camber gauges
- Surface-roughness testers
- Coating-thickness gauges
Thickness should be measured at several positions rather than at only one edge. For coil and strip products, the inspection plan may also include width, camber, burr height, edge condition, coil inner diameter and coil weight.
JUDE provides
stainless steel sheet and plate
,
stainless steel coil
and
precision stainless steel strip
with customized dimensions and surface finishes.
2. Check the Material Test Certificate
A material test certificate, mill test certificate or MTC is one of the most important documents in stainless steel purchasing. A typical certificate identifies the material grade, product standard, heat number, chemical composition and mechanical properties.
Information to Verify on the Certificate
- Manufacturer or steel mill
- Customer or purchase-order reference
- Grade and UNS, EN or JIS designation
- Applicable product standard
- Heat number or melt number
- Product dimensions and quantity
- Chemical composition
- Tensile strength and yield strength
- Elongation and hardness where required
- Heat-treatment condition
- Required corrosion or supplementary tests
- Authorized inspection signature or validation
A certificate is not sufficient if the heat number on the document cannot be matched to the product, label, packaging or individual component.
For higher-risk projects, buyers may request an EN 10204 3.1 certificate, independent third-party inspection, witness testing or additional product analysis.
Available JUDE documentation can be reviewed on the
inspection report and certification page
.
3. Can You Test Stainless Steel With a Magnet?
A magnet test is fast and inexpensive, but it is only a screening method. Magnetic response is controlled mainly by metallurgical structure and processing condition rather than by the word “stainless.”
| Stainless Steel Family | Typical Magnetic Response | Examples |
|---|---|---|
| Austenitic | Usually non-magnetic or weakly magnetic when annealed | 304, 304L, 316L, 317L |
| Ferritic | Magnetic | 409, 430, 439, 441, 444 |
| Martensitic | Magnetic | 410, 420, 420J2, 440C |
| Дуплекс | Magnetic | 2101, 2205, 2507 |
| Precipitation hardening | Often magnetic | 17-4PH, 15-5PH |
Cold forming, rolling, bending and machining can make austenitic stainless steel more magnetic. Weld metal may also display a magnetic response because of ferrite or transformation created during fabrication.
A magnet cannot reliably distinguish 304 from 316, 304 from 304L or many other closely related grades.
4. Spark Testing
Spark testing involves touching the metal to a grinding wheel and observing spark color, length, branching and intensity. Experienced operators may use the pattern to make a rough distinction between carbon steel, stainless steel and certain alloy families.
High-carbon steels tend to produce more branching sparks, while many austenitic stainless steels produce fewer and darker sparks. However, alloy condition, wheel type, grinding pressure, lighting and operator experience can affect the observation.
Why Spark Testing Has Limited Value
- It is subjective.
- Closely related stainless grades may have similar patterns.
- It removes material and damages the surface.
- It may contaminate stainless steel with carbon-steel particles.
- It cannot provide a quantitative chemical composition.
- It is inappropriate for clean, finished or safety-critical parts.
Spark testing can be used for preliminary workshop sorting, but PMI or laboratory analysis should be used for final grade verification.
5. Chemical Spot Testing
Chemical spot-test kits use reagents that react with selected alloying elements. One common application is screening for molybdenum to help separate many 304-type materials from 316-type materials.
A spot test can be useful when:
- A handheld analyzer is not available
- Only a small number of items need screening
- The goal is to determine whether molybdenum is likely to be present
- The result will be confirmed by another method when necessary
Limitations of Chemical Spot Tests
- Results are often qualitative or semi-quantitative.
- Surface coatings, contamination and oxide can interfere.
- Correct surface preparation is required.
- Reagents may be hazardous and require controlled handling.
- A positive molybdenum result does not independently prove a specific grade.
- Spot tests normally cannot confirm low-carbon grades.
6. PMI and Handheld XRF Testing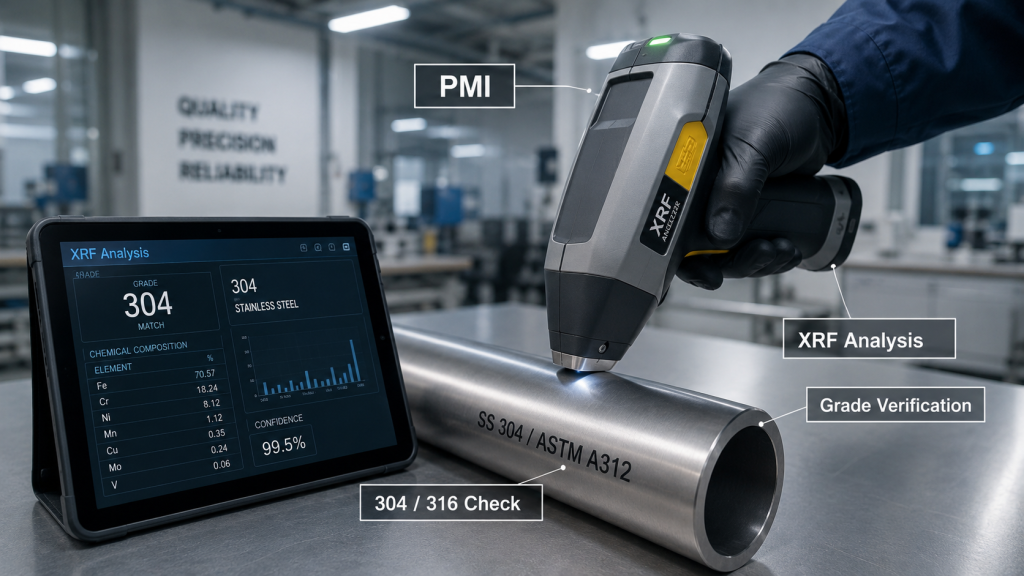 PMI verifies that the nominal alloy composition matches the specified stainless steel grade.
Positive material identification, or PMI, is a quality-assurance process used to verify alloy composition and prevent material mix-ups. PMI may include handheld XRF, LIBS, OES or another suitable analytical method.
How Handheld XRF Works
X-ray fluorescence exposes the surface to X-rays and measures the characteristic fluorescent energy emitted by the elements in the material.
Handheld XRF is commonly used to identify:
- Chromium
- Nickel
- Molybdenum
- Manganese
- Niobium
- Titanium
- Copper
- Cobalt
- Tungsten and other heavier alloying elements
Advantages of XRF Testing
- Rapid field analysis
- Little or no visible surface damage
- Portable testing of sheet, pipe, valves, fittings and installed equipment
- Useful separation of 304 and 316 through molybdenum detection
- Useful identification of 2205, 2507, 904L and nickel alloys
- Digital test records and alloy-library comparison
Limitations of XRF
Conventional handheld XRF cannot directly measure carbon. It therefore cannot reliably distinguish grades whose primary difference is carbon content.
| Grade Comparison | Can XRF Usually Separate Them? | Reason |
|---|---|---|
| 304 vs 316 | Usually yes | 316 normally contains molybdenum |
| 304 vs 304L | Not reliably | The main difference is carbon |
| 316 vs 316L | Not reliably | The main difference is carbon |
| 321 vs 304 | Usually possible | 321 contains intentional titanium |
| 347 vs 304 | Usually possible | 347 contains intentional niobium |
| 304 vs 2205 | Usually yes | Substantially different Cr, Ni, Mo and often N requirements |
| 316L vs 904L | Usually yes | 904L contains much higher nickel, molybdenum and copper |
XRF is surface-sensitive. Paint, plating, heavy oxide, corrosion products, dirt and transferred metal can distort results. The surface may require cleaning or controlled grinding before analysis.
Handheld XRF instruments emit ionizing radiation and must only be used by trained personnel in accordance with local radiation-safety requirements.
7. OES, LIBS and Laboratory Chemical Analysis
Spark Optical Emission Spectroscopy
Spark optical emission spectroscopy, commonly called spark OES, creates an electrical discharge on a prepared metal surface. The emitted light is separated into wavelengths that correspond to individual elements.
OES can measure carbon and other elements that conventional handheld XRF cannot measure directly. It is therefore useful for differentiating:
- 304 from 304L
- 316 from 316L
- Low-carbon and standard-carbon stainless grades
- Carbon-controlled martensitic grades
- Duplex grades requiring nitrogen verification
OES requires a clean, flat and properly prepared test surface. The spark leaves a small burn mark, so test location should be agreed before testing finished components.
Laser-Induced Breakdown Spectroscopy
LIBS uses a focused laser pulse to create a small plasma on the surface. The emitted spectrum is analyzed to identify the alloy chemistry.
Suitable handheld LIBS instruments can measure carbon at low concentrations and may be used for field separation of L-grade stainless steels. Performance depends on calibration, surface preparation, test atmosphere, reference materials and operator procedure.
Combustion Analysis
Carbon and sulfur can be measured by combustion analysis. A representative sample is burned under controlled conditions, and the resulting gases are measured.
This method is commonly used when an accurate carbon result is necessary to verify a low-carbon stainless steel grade.
ICP-OES and Wet Chemical Analysis
Inductively coupled plasma optical emission spectroscopy and other laboratory chemical methods can provide highly detailed elemental analysis. The sample must normally be dissolved or otherwise prepared before measurement.
Independent laboratory analysis is appropriate when:
- A purchase dispute exists
- A complete product analysis is required
- Trace or residual elements must be measured
- Safety-code compliance is critical
- A low-carbon grade must be confirmed independently
- The customer requires third-party certification
8. Mechanical Testing
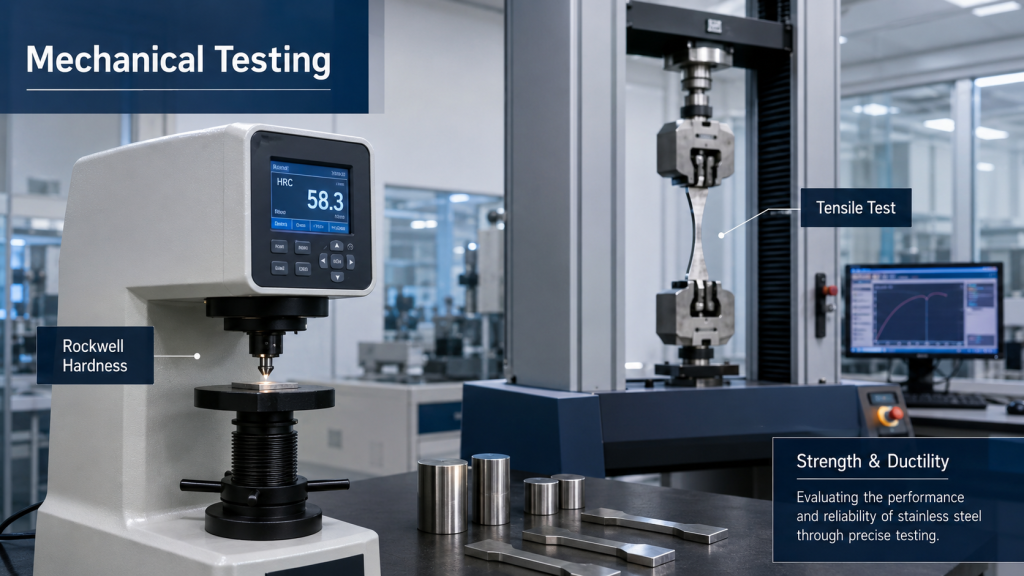 Mechanical testing confirms the delivered condition, strength, ductility and hardness of stainless steel products.
Hardness Testing
Hardness testing measures resistance to indentation. It is useful for confirming heat-treatment condition, cold-work level and production consistency.
Common hardness methods include:
- Rockwell: fast testing for many production components
- Brinell: larger indentation suited to thicker or less uniform material
- Vickers: useful over a wide hardness range and for thinner sections
- Microhardness: used for small regions, coatings or hardness profiles
- Portable hardness testing: used when the component cannot be placed on a laboratory machine
Hardness does not independently identify stainless steel grade. Different grades and processing conditions can produce overlapping hardness values.
Examples of Useful Hardness Checks
- Confirming annealed 304 or 316L sheet condition
- Checking cold-rolled strip hardness
- Verifying quenched and tempered 420 or 440C
- Confirming aged 17-4PH condition
- Identifying local weld or heat-affected-zone hardening
Tensile Testing
A tensile test pulls a standardized specimen until failure. It can determine:
- Yield strength
- Ultimate tensile strength
- Elongation
- Reduction of area
- Stress-strain behavior
Tensile testing is destructive and requires a specimen with the correct orientation and geometry. Results must be compared with the applicable product standard, thickness range and delivery condition.
Bend, Impact and Flattening Tests
Depending on product form and project requirements, stainless steel may also be tested by:
- Guided bend testing
- Charpy impact testing
- Tube flattening
- Tube flaring
- Reverse-bend testing
- Fatigue testing
The correct test method must be selected from the applicable sheet, plate, bar, tube, pipe, forging, casting or welding specification.
9. Metallographic and Microstructural Testing
Metallography examines a prepared and etched cross-section under an optical or electron microscope. It provides information that cannot be obtained from surface appearance or basic PMI.
Metallographic examination can evaluate:
- Austenitic, ferritic, martensitic or duplex structure
- Grain size
- Ferrite-austenite phase balance
- Carbide precipitation
- Sigma phase or other detrimental intermetallic phases
- Decarburization
- Inclusions and cleanliness
- Weld penetration and fusion
- Heat-affected-zone condition
- Crack origin and failure mechanism
Duplex Stainless Steel Testing
Duplex grades such as
duplex 2205
and
super duplex 2507
require more than simple grade identification.
Welding and thermal processing can change ferrite-austenite balance or form detrimental phases. Depending on the specification, testing may include metallography, ferrite measurement, impact testing and corrosion testing.
10. Surface Finish, Cleanliness and Passivation Testing
Surface condition has a major influence on appearance, cleanability and corrosion performance. Correct alloy chemistry does not compensate for severe iron contamination, rough welds, heat tint or improper cleaning.
Surface Roughness Testing
A profilometer can measure surface parameters such as Ra and Rz. The required value depends on the drawing, customer specification and application.
Pharmaceutical, food-processing and sanitary equipment may require a controlled finish because rough surfaces can retain deposits and become difficult to clean.
Free-Iron Contamination Testing
Stainless steel can develop rust stains when carbon-steel particles are transferred during grinding, handling, blasting or storage.
Project-specified free-iron tests can help determine whether the surface is contaminated. Cleaning, pickling and passivation procedures should be selected according to the product, finish and service requirements.
Water-Break Testing
A water-break test may be used as a simple check for oily or hydrophobic contamination. A clean surface normally supports a more continuous water film, while contamination can cause the water to separate into droplets.
Passivation Verification
Passivation verification does not prove the full alloy grade. It checks whether the processed stainless steel surface satisfies the selected acceptance procedure.
ASTM A380/A380M and ASTM A967/A967M are commonly referenced for cleaning, descaling, pickling, passivation treatments and associated verification requirements.
11. Stainless Steel Corrosion Testing
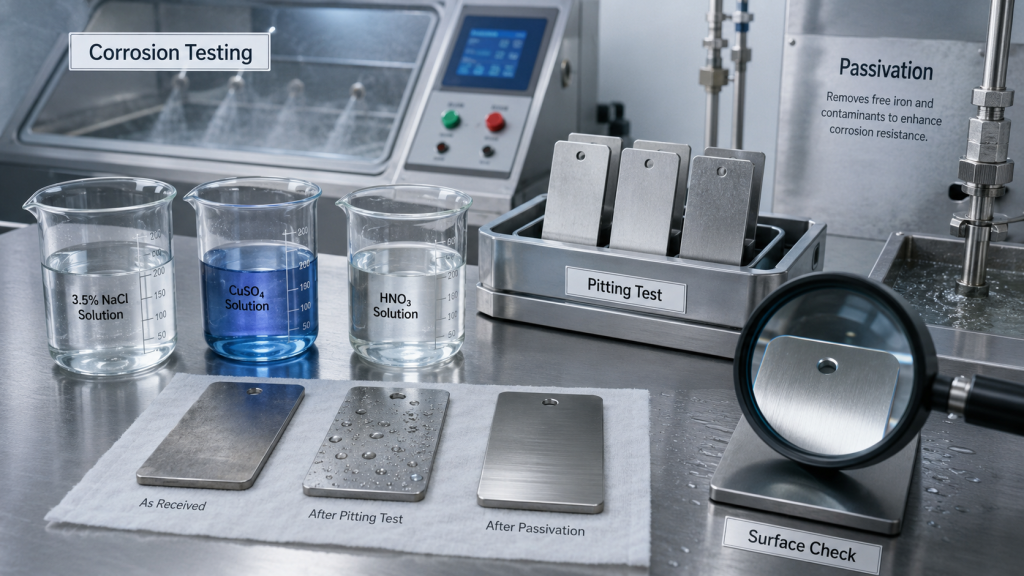
Corrosion tests compare material performance under defined laboratory conditions and must be matched to the alloy family and service risk.
ASTM G48 Pitting and Crevice Corrosion Testing
ASTM G48 uses ferric chloride solutions to evaluate resistance to pitting and crevice-corrosion initiation under specified conditions.
The standard includes methods for:
- Pitting testing
- Crevice-corrosion testing
- Critical pitting temperature
- Critical crevice temperature
G48 is frequently used for duplex, super duplex, high-alloy austenitic stainless steel and nickel alloys.
ASTM G48 is a controlled comparative test. Passing one procedure does not mean that the material will resist every industrial chemical or natural seawater condition.
Intergranular Corrosion Testing
Austenitic stainless steels may be evaluated for susceptibility to intergranular attack using practices such as ASTM A262.
Intergranular corrosion testing is particularly relevant when welding or thermal exposure may have caused sensitization and chromium-carbide precipitation.
Duplex Stainless Steel Corrosion and Phase Testing
Duplex grades may be evaluated using ASTM A923 or other project-specified methods to detect detrimental intermetallic phases and verify processing quality.
Salt Spray Testing
Salt spray testing exposes samples to a controlled salt-fog environment. It is useful for evaluating coatings, finishes, comparative processes or customer-defined acceptance requirements.
Salt spray duration should not be treated as a universal prediction of stainless steel service life. Natural environments involve temperature cycles, drying, deposits, crevices, pollution and cleaning conditions that may not be represented by a continuous laboratory fog.
Application-Specific Immersion Testing
For critical chemical equipment, the most relevant test may use the actual or simulated process liquid at the operating concentration and temperature.
The test plan may consider:
- General mass-loss corrosion rate
- Pitting depth and density
- Crevice geometry
- Welded and unwelded specimens
- Heat-affected zones
- Flow or agitation
- Aeration and oxygen content
- Contaminants and deposits
12. Nondestructive Testing of Stainless Steel
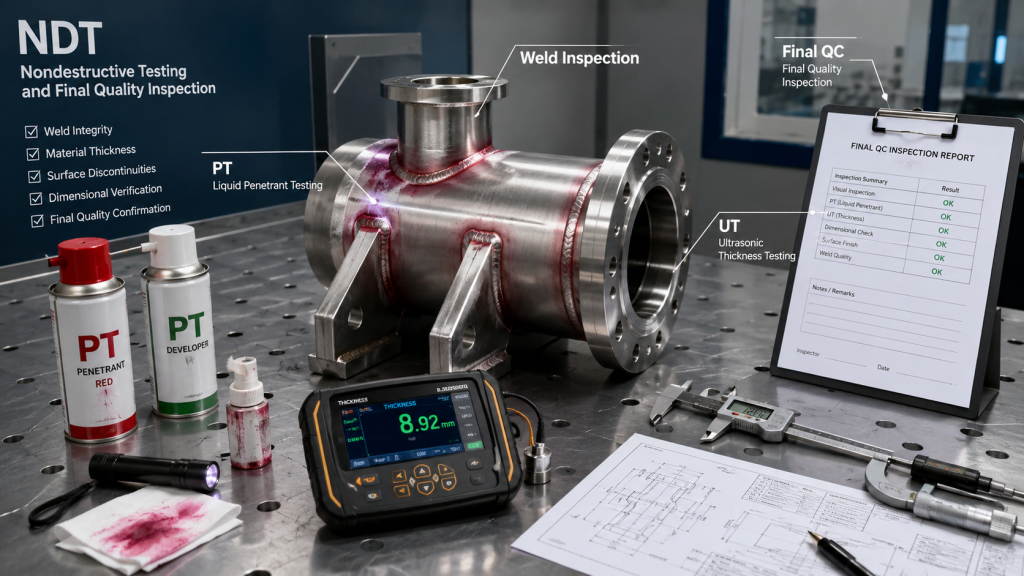
Nondestructive testing detects surface or internal discontinuities without destroying the finished component.
Liquid Penetrant Testing
Liquid penetrant testing is widely used for detecting surface-breaking discontinuities in nonporous stainless steel components and welds.
A typical sequence includes:
- Pre-cleaning
- Penetrant application
- Specified penetration time
- Removal of excess penetrant
- Developer application
- Inspection under the required lighting
- Interpretation and reporting
- Post-cleaning where required
Penetrant testing can reveal cracks, laps, seams and open porosity, but it cannot detect defects that do not connect to the surface.
Magnetic Particle Testing
Magnetic particle testing is limited to ferromagnetic materials. It can be applied to ferritic, martensitic and many duplex stainless steels, but it is normally unsuitable for fully austenitic stainless steel.
It can detect discontinuities at or near the surface, including certain cracks in welds, forgings and heat-treated components.
Ultrasonic Testing
Ultrasonic testing introduces high-frequency sound into the material. Reflections can be used to measure thickness or locate internal discontinuities.
Typical applications include:
- Plate-lamination inspection
- Pipe and tube wall-thickness measurement
- Weld inspection
- Corrosion mapping
- Forging inspection
Radiographic Testing
Radiographic testing uses X-rays or gamma rays to create an image of internal features. It is commonly used for selected welds, castings and pressure-retaining components.
Radiography requires controlled radiation safety, a qualified written procedure and trained personnel.
Eddy Current Testing
Eddy current testing uses electromagnetic induction and is especially useful for examining conductive materials such as stainless steel tubing.
It can detect certain surface and near-surface defects, dimensional changes and material variations. Calibration standards must represent the product and expected defect type.
How to Identify Common Stainless Steel Grades
How to Test 304 vs 316 Stainless Steel
Grade 304 and 316 normally look almost identical. A magnet test cannot reliably separate them.
The most practical field method is handheld XRF or a validated molybdenum spot test. Grade 316 normally contains approximately 2–3% molybdenum, while standard 304 does not contain an intentional molybdenum addition.
Read JUDE’s
304 stainless steel guide
and
316L material page
for additional grade information.
How to Test 304 vs 304L
The main difference is carbon content. Conventional handheld XRF cannot directly measure carbon and therefore cannot reliably separate 304 from 304L.
Use one or more of the following:
- Heat-number traceability and MTC verification
- Spark OES
- Carbon-capable handheld LIBS
- Laboratory combustion analysis
For more detail, read
304 vs 304L stainless steel
.
How to Test 316 vs 316L
The same limitation applies to 316 and 316L. Their chromium, nickel and molybdenum ranges can overlap, while the primary specification difference is maximum carbon.
XRF can usually identify the material as a 316-type alloy but cannot independently verify that it satisfies the low-carbon requirement.
How to Test 304 vs 430
Annealed 304 is usually non-magnetic or only weakly magnetic, while
430 stainless steel
is ferritic and strongly magnetic.
A magnet may provide a quick preliminary indication, but XRF should be used when grade confirmation is required because cold-worked 304 can also display magnetism.
How to Test 316L vs Duplex 2205
Duplex 2205 is magnetic and normally contains higher chromium, lower nickel and a controlled nitrogen addition compared with 316L.
XRF can usually distinguish the alloy families, but full duplex acceptance may also require OES or laboratory nitrogen analysis, ferrite measurement, mechanical testing and verification that no detrimental phases were created during fabrication.
Testing Stainless Steel by Product Form
| Product Form | Recommended Incoming Checks | Possible Additional Tests |
|---|---|---|
| Sheet and plate | MTC, heat number, dimensions, flatness, surface, PMI | UT, tensile, hardness, corrosion and roughness |
| Coil | MTC, thickness, width, coil weight, surface, edge and PMI | Camber, crown, hardness profile and mechanical tests |
| Precision strip | Thickness mapping, width, burr, edge, hardness and surface | Tensile, bend, flatness and roughness |
| Pipe and tube | Grade, dimensions, wall thickness, visual inspection and PMI | Eddy current, hydrostatic, UT, flattening and flare tests |
| Bar and rod | Grade, diameter, straightness, surface and PMI | Hardness, UT, tensile and macrostructure |
| Welded fabrication | Base-metal and filler traceability, dimensions and visual weld inspection | PT, RT, UT, ferrite, hardness and corrosion testing |
| Heat-treated component | Grade, heat-treatment records, dimensions and hardness | Metallography, tensile, impact and corrosion tests |
A Practical Stainless Steel Incoming Inspection Workflow
Review the Purchase Specification
Confirm the required grade, standard, product form, dimensions, finish, mechanical properties, testing, certificates and acceptance criteria.
Inspect Packaging and Identification
Check labels, grade markings, heat numbers, pallet condition, moisture damage and shipping documentation.
Match the Heat Number to the MTC
Verify that the product, packaging and certificate reference the same heat or batch.
Review Chemical and Mechanical Results
Compare the certified values with the applicable product standard and any project-specific requirements.
Perform Visual Inspection
Check surface finish, rust, scratches, dents, edge damage, laminations, weld condition and contamination.
Measure Dimensions
Record thickness, width, length, diameter, flatness, camber or other specified dimensions at representative locations.
Perform PMI
Use XRF, LIBS, OES or another approved method according to the grade, required elements and inspection plan.
Confirm Low-Carbon Grades When Required
Do not rely on XRF alone for 304L, 316L or another carbon-controlled grade. Verify carbon by traceability or a carbon-capable method.
Complete Mechanical or Corrosion Tests
Perform hardness, tensile, impact, G48, intergranular corrosion or other tests when required by the order.
Complete Nondestructive Examination
Apply PT, UT, RT, eddy current or another specified examination to the appropriate product or weld.
Document Nonconformities
Isolate rejected or questionable material and record the heat number, location, test result, photographs and disposition.
Release and Maintain Traceability
Protect grade and heat-number identification during cutting, slitting, fabrication, storage and delivery.
Common Standards Used for Stainless Steel Testing
| Стандарт | General Purpose |
|---|---|
| ASTM E1086 | Analysis of austenitic stainless steel by spark atomic emission spectrometry |
| ASTM E572 | Analysis of stainless and alloy steels by wavelength-dispersive XRF |
| ASTM E1019 | Carbon, sulfur, nitrogen and oxygen determination in steels and related alloys |
| ASTM E18 | Rockwell hardness testing |
| ASTM E10 | Brinell hardness testing |
| ASTM E92 | Vickers and Knoop hardness testing |
| ASTM E8/E8M | Tensile testing of metallic materials |
| ASTM G48 | Pitting and crevice corrosion resistance using ferric chloride |
| ASTM A262 | Susceptibility to intergranular attack in austenitic stainless steels |
| ASTM A923 | Detection of detrimental intermetallic phases in duplex stainless steels |
| ASTM A763 | Intergranular corrosion susceptibility of ferritic stainless steels |
| ASTM A380/A380M | Cleaning, descaling, pickling and passivation practices |
| ASTM A967/A967M | Chemical passivation treatments for stainless steel parts |
| ASTM E165/E165M | Liquid penetrant testing for general industry |
| ASTM E709 | Magnetic particle testing guidance for ferromagnetic materials |
| API RP 578 | Material verification programs and PMI for new and existing assets |
Standards are revised periodically. Always confirm the edition specified by the contract, design code, purchase order or regulatory authority before testing.
Common Stainless Steel Testing Mistakes
Using Only a Magnet
Magnetic response identifies approximate metallurgical behavior, not a unique chemical grade.
Assuming XRF Can Measure Carbon
Conventional handheld XRF cannot verify the low-carbon requirement of 304L, 316L or similar grades.
Testing Through Paint or Heavy Scale
Coatings, corrosion products and contamination can distort surface-analysis results.
Testing Only One Location
A single reading may miss mixed batches, substituted fittings, incorrect weld filler or local variation.
Ignoring Calibration and Reference Materials
Instruments must be calibrated, verified and used within their suitable analytical range.
Accepting a Certificate Without Traceability
The certificate must correspond to the actual heat number and delivered product.
Using Hardness as Proof of Grade
Hardness can confirm material condition but does not independently establish chemical composition.
Using Salt Spray Hours as Universal Service Life
Accelerated tests are comparative tools and do not reproduce every industrial or natural environment.
Failing to Control Test Location
Welds, base metal, coatings and heat-affected zones may produce different readings. The test location must match the inspection objective.
Stainless Steel Purchasing and Inspection Checklist
Provide the following information when requesting stainless steel and testing support:
- Grade: Specify the complete designation, such as 304L/S30403 or 2205/S32205.
- Standard: Identify ASTM, ASME, EN, JIS or another required product standard.
- Product form: Sheet, plate, coil, strip, tube, pipe, bar or fabricated part.
- Dimensions: Thickness, width, length, diameter and tolerances.
- Surface finish: No.1, 2B, BA, No.4, hairline, mirror or custom finish.
- Edge condition: Mill edge, slit edge, deburred edge or rounded edge.
- Mechanical properties: Tensile, yield, elongation, hardness or impact requirements.
- Chemical requirements: Standard limits and any tighter project restrictions.
- PMI scope: Test method, sampling percentage, locations and acceptance criteria.
- Corrosion testing: Specify G48, intergranular or project-specific immersion tests.
- NDT: PT, MT, UT, RT or eddy-current requirements.
- Documentation: MTC, inspection report, PMI report and third-party certification.
- Marking: Grade, heat number, dimensions and traceability requirements.
- End application: Explain the corrosive environment, temperature and fabrication process.
- Destination: Quantity, delivery schedule, packaging and destination port.
How JUDE Supports Stainless Steel Quality Verification
JUDE supplies stainless steel sheet, plate, coil and precision strip with material traceability, inspection documentation and customized processing.
Available support may include:
- Material certificate review
- Heat-number traceability
- Dimensional and surface inspection
- PMI and chemical-composition verification
- Mechanical-property testing
- Customized third-party inspection
- Cut-to-length and precision slitting
- Deburred and rounded-edge processing
- Surface polishing and protective-film application
- Export packaging and inspection documentation
JUDE’s
stainless steel strip-processing service
covers uncoiling, slitting, leveling, rewinding and customized packaging.
For customized components, JUDE also provides services such as
waterjet cutting
and other stainless steel processing solutions.
Final Conclusion
Testing stainless steel is not one individual test. It is a verification system combining documentation, traceability, visual inspection, dimensional measurement, material identification, mechanical-property testing, corrosion evaluation and nondestructive examination.
Magnet and spark tests can provide preliminary information, but they cannot reliably confirm a specific stainless steel grade.
Handheld XRF is one of the most efficient methods for rapid field PMI because it can identify important alloying elements such as chromium, nickel and molybdenum. However, it cannot directly measure carbon and should not be used alone to confirm 304L, 316L or another low-carbon grade.
For critical applications, combine heat-number traceability with the correct analytical method, mechanical testing, corrosion testing and NDT required by the product standard and project specification.
Frequently Asked Questions
How can I tell whether a metal is stainless steel?
Start with markings, visual inspection and a magnet test, but use PMI, XRF, OES, LIBS or laboratory chemical analysis when reliable identification is required. Appearance alone cannot prove that a metal is stainless steel.
Can a magnet identify stainless steel grade?
No. A magnet can indicate magnetic response and help separate some alloy families, but it cannot reliably identify a specific grade. Cold-worked austenitic stainless steel may also become magnetic.
What is the best field test for stainless steel?
Handheld XRF is one of the most practical field methods for PMI and alloy identification. It should be combined with certificate and heat-number verification.
Can XRF identify stainless steel?
Yes. XRF can identify many stainless steel grades by measuring elements such as chromium, nickel, molybdenum and manganese. Its limitations must be considered for carbon-controlled grades.
Can XRF distinguish 304 from 316 stainless steel?
Usually yes. Grade 316 normally contains approximately 2–3% molybdenum, while standard 304 does not contain an intentional molybdenum addition.
Can XRF distinguish 304 from 304L?
Not reliably. The primary difference is carbon content, and conventional handheld XRF cannot directly measure carbon. Use traceability, OES, carbon-capable LIBS or combustion analysis.
Can XRF distinguish 316 from 316L?
Not reliably. XRF can identify the material as a 316-type alloy, but it cannot independently confirm the lower carbon limit required for 316L.
What is PMI testing?
Positive material identification is a process used to verify that an alloy has the nominal chemical composition required by the specification. PMI may use XRF, LIBS, OES or another approved method.
Does stainless steel always pass a magnet test?
There is no universal pass or fail response. Ferritic, martensitic and duplex grades are magnetic. Annealed austenitic grades are usually non-magnetic or weakly magnetic, but cold working can increase magnetism.
How is stainless steel hardness tested?
Stainless steel can be tested using Rockwell, Brinell, Vickers, Knoop or suitable portable hardness methods. The selected scale depends on material condition, thickness and expected hardness.
How do you test stainless steel corrosion resistance?
The appropriate method depends on the corrosion mechanism. Examples include ASTM G48 for pitting and crevice corrosion, ASTM A262 for intergranular attack and application-specific immersion testing.
Can stainless steel be tested without damaging it?
Yes. Visual inspection, dimensional measurement, handheld XRF, ultrasonic testing, eddy current and some other NDT methods cause little or no damage. OES, hardness indentation and laboratory sampling create a mark or require material removal.
What should be checked on a stainless steel certificate?
Check the steel mill, grade, standard, heat number, dimensions, chemical composition, mechanical properties, heat-treatment condition and required supplementary tests. The certificate must match the markings on the delivered material.
Should stainless steel be tested before purchase?
Critical orders should define the inspection and testing requirements before production. Buyers should verify certificates, heat numbers, dimensions, surface quality and grade consistency before accepting the shipment.
Which test is required for safety-critical stainless steel?
There is no single universal test. The inspection package must be based on the product standard, design code, service environment and consequences of failure. It may include full traceability, PMI, laboratory chemistry, mechanical tests, corrosion tests and NDT.
Request Stainless Steel Testing and Supply Support
Send JUDE your required grade, product standard, dimensions, quantity, surface finish, PMI scope, mechanical requirements, corrosion testing, inspection documents and destination port.
For critical chemical, marine, pressure-retaining or welded applications, include the operating environment and project specification so the appropriate material and inspection plan can be reviewed.
